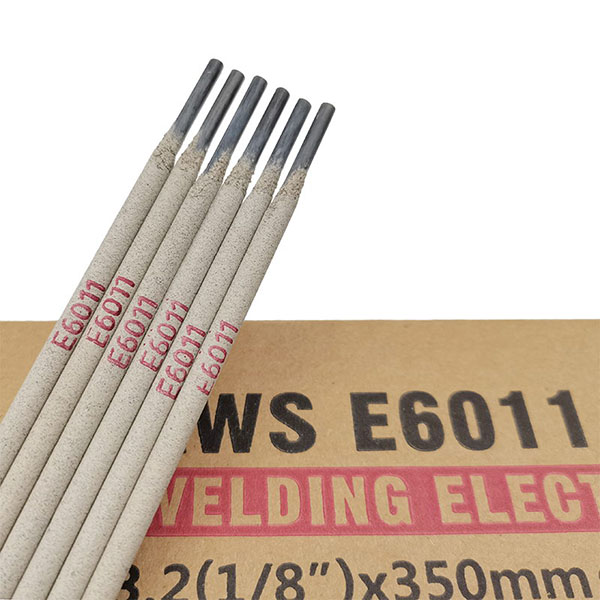
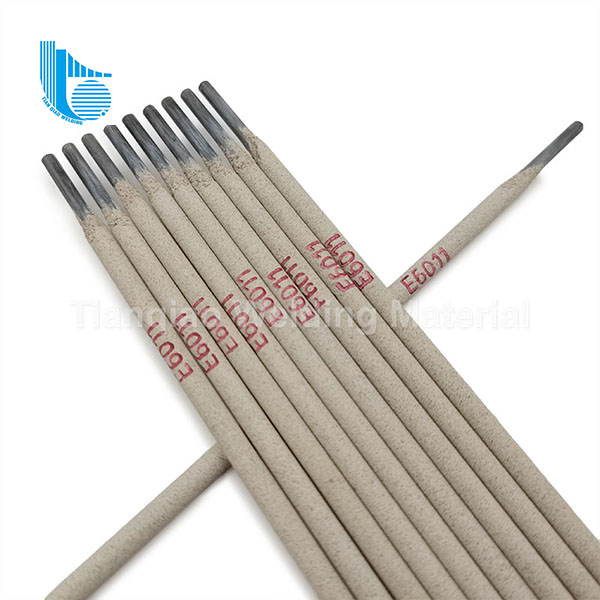
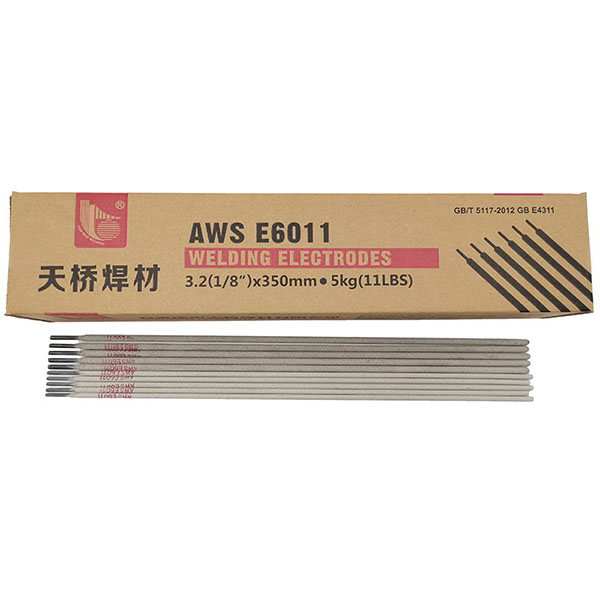
✓
APPLICATIONS
It is suitable for welding of low carbon steel structure as pipeline, shipbuilding and etc.
★
CHARACTERISTICS
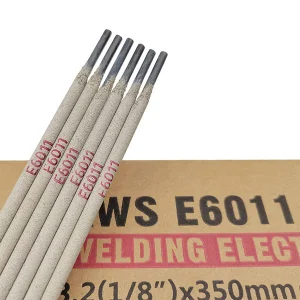
E6011 is a rutile-cellulosic potassium type electrode. Can be weld for all-position (especially for vertical-down position) with AC and DC+. It have excellent welding performance as stable arc, little spatter, easy slag removal and reigniting-ability etc. Also it has advantages of better molten pool control, stronger arc force and deeper penetration at vertical-down position.
!
ATTENTION
1. In generally, don't need to re-dry the electrode before welding. When it be affected with damp, should be re-dry it at 70℃-90℃ for 1 hour.
2. The rust, oil, water and other impurities of the weld area must be removed before welding.
⊕
WELDING POSITIONS
Positions: PA, PB, PC, PD, PE, PF
X-ray flaw detection: Ⅱ level
⚓
DEPOSIT COMPOSITION (Quality Score): %
| Items |
C |
Mn |
Si |
S |
P |
Ni |
Cr |
Mo |
V |
| Requirements |
≤0.20 |
≤1.20 |
≤1.00 |
≤0.035 |
≤0.040 |
≤0.30 |
≤0.20 |
≤0.30 |
≤0.08 |
| Typical Results |
0.09 |
0.42 |
0.15 |
0.020 |
0.025 |
0.030 |
0.035 |
0.005 |
0.004 |
⚙
MECHANICAL PROPERTIES
| Items |
Tensile Strength Rm/MPa |
Yield Strength Rel/Rp0.2 MPa |
Elongation A/% |
Charpy V-Notch KV2(J)-30℃ |
| Requirements |
≥430 |
≥330 |
≥20 |
≥27 |
| Typical Results |
475 |
400 |
26 |
80 |
⚡
TYPICAL OPERATING PROCEDURES: (AC,DC+)
| Diameter (mm) |
2.5 |
3.2 |
4.0 |
5.0 |
| Current (A) |
40-60 |
80-100 |
100-140 |
150-200 |
📦
PACKAGING & OEM/ODM
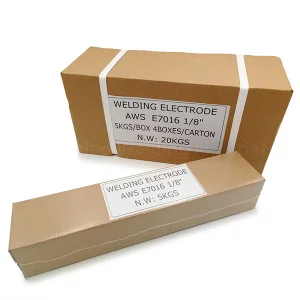
Standard Packaging: 5kgs/box, 4boxes/carton, 20kgs/carton, 50cartons/pallet. 21-26MT per 1X20" FCL.
Customization: We support OEM/ODM and could make packaging according to your design, please contact us for detail discussion.
?
Frequently Asked Questions
Q1: What are the primary applications for E6011 electrodes?
A: E6011 is ideally suited for welding low carbon steel structures, specifically pipelines, shipbuilding, and general steel fabrication.
Q2: Can E6011 be used for vertical-down welding?
A: Yes, it is designed for all-position welding and is particularly effective for vertical-down positions due to its strong arc force and excellent molten pool control.
Q3: Do I need to dry the E6011 electrodes before use?
A: Generally, re-drying is not required. However, if the electrodes become damp, they should be re-dried at 70℃-90℃ for approximately 1 hour.
Q4: What type of power source is required for E6011?
A: These electrodes are compatible with both AC and DC+ (Direct Current Positive) welding power sources.
Q5: What is the typical tensile strength of the E6011 weld?
A: The typical tensile strength result for E6011 is 475 MPa, which exceeds the minimum requirement of 430 MPa.
Q6: Is customized packaging available for bulk orders?
A: Yes, we provide full OEM/ODM services and can customize packaging and design based on your specific requirements.
 Tianqiao Welding